Key Takeaways
- Ethanol distillery machinery selection directly affects ethanol production cost, energy consumption, DSCR, IRR, and long-term profitability for Indian grain-based ethanol plants. Projects targeting an internal rate of return of 15–20% cannot afford inefficient or poorly matched equipment.
- A modern grain-based ethanol manufacturing plant with capacities ranging from 60 to 200 KLPD typically includes grain handling, fermentation, distillation columns, molecular sieve dehydration, DDGS drying, boilers, utilities, ETP, and automation systems – each stage requiring specialised machinery to optimise efficiency.
- Ethanol distillery machinery cost in India must be evaluated at three levels: ex-works equipment price, installed plant machinery cost (including freight, GST, erection, piping, and instrumentation), and total project investment including civil works, utilities, and pre-operative expenses.
- Project Report Bank, led by CA Manish Gugliya, helps promoters integrate machinery choices into bankable DPRs, project planning, feasibility studies, and project economics for ethanol plant finance.
- All cost ranges presented here are indicative budgeting norms valid for India around FY 2025–26. They must be validated with current supplier quotations and a detailed feasibility study before committing capital.
Introduction – Ethanol Distillery Machinery & Investment Planning
India’s ethanol blending roadmap towards E20 by 2025–26 has created sustained demand for efficient ethanol distillery machinery across the country. With the global ethanol market size at USD 104.80 billion in 2025 and expected to reach USD 158.45 billion by 2034, the investment opportunity is substantial – but so are the risks of poorly planned projects.
Ethanol production is a multi-step industrial process involving feedstock preparation, fermentation, and distillation. Starch-rich biomass such as corn and sugarcane is commonly used, and ethanol can be produced from corn, sugarcane, and other grains. In India, grain-based ethanol plants using maize and broken rice have become the dominant new-capacity additions. Ethanol production converts biomass into alcohol through fermentation and thermal separation, and ethanol production plants typically use fermentation and distillation processes to produce ethanol at fuel grade.
The entire process from grain intake to fuel-grade ethanol and distillers dried grains depends on technology selection that directly determines ethanol recovery per tonne of feedstock, steam consumption (typically 3.0–4.5 kg per litre for grain-based plants), and energy consumption (0.35–0.55 kWh per litre). These factors shape ethanol production cost per litre, by-product revenue, and ultimately whether a project can service its debt.
Typical plant capacity ranges in India include 60, 100, 160, and 200 KLPD. Ethanol plant setup costs range from INR 50–600 crore depending on capacity, feedstock, and environmental configuration. Capital costs for grain-based plants range from INR 100–600 crore, higher than molasses-based facilities due to grain handling systems. This article, written in an advisory capacity by CA Manish Gugliya of Project Report Bank, focuses on practical machinery and cost insights for ethanol plant promoters – not on selling equipment.
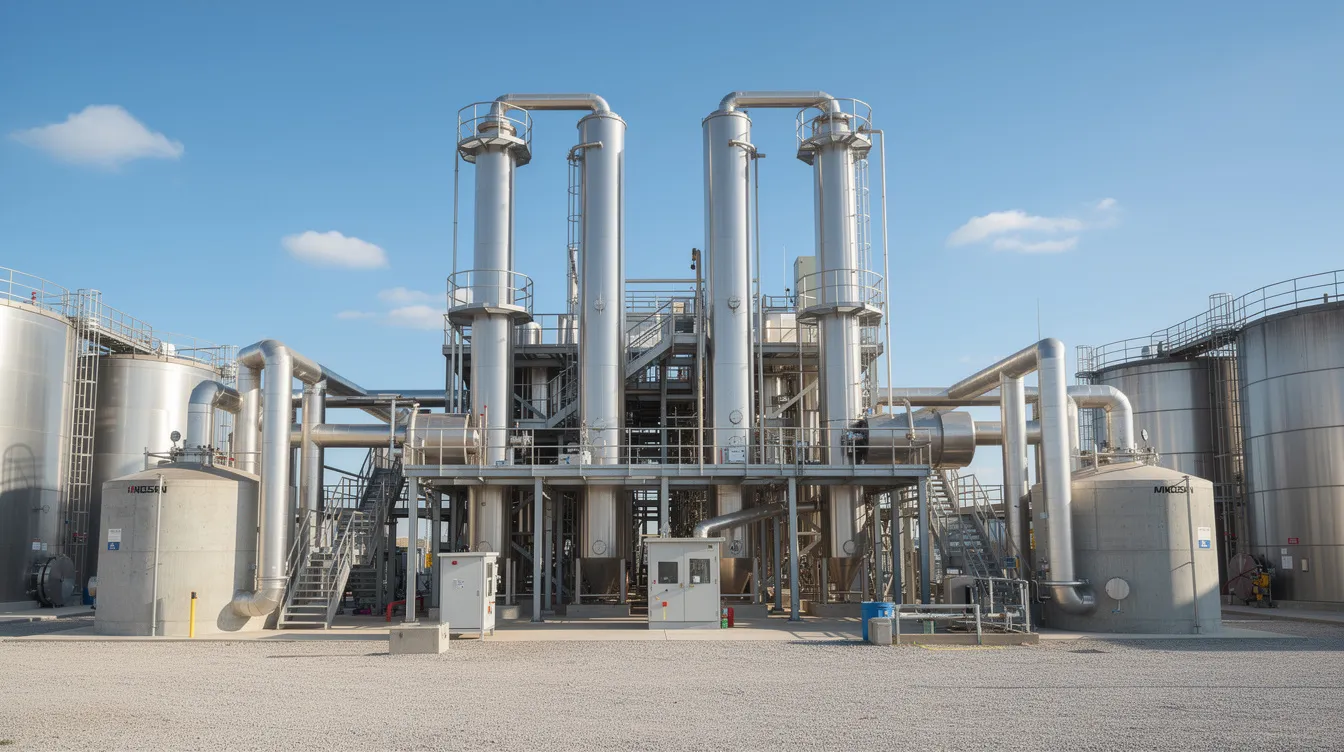
Complete Ethanol Distillery Machinery & Equipment List
The following table covers key equipment for grain-based fuel ethanol plants processing maize, broken rice, or damaged foodgrains. Feedstock selection significantly impacts plant configuration and costs. Molasses-based or sugarcane juice-based facilities differ in the front-end; cellulosic biomass plants differ substantially throughout. Dual feed configurations allow switching between molasses and grain feedstocks but require additional process flexibility. Ethanol plants can process various feedstocks including corn and sugarcane, and plants handling sweet sorghum or cassava will need modified pre-treatment. Each stage of ethanol production requires specialised machinery to optimise efficiency.
| Machinery / Equipment | Main Function | Technical Selection Considerations |
|---|---|---|
| Grain cleaning and milling system | Feedstock preparation | Throughput (TPD), particle size 0.5–1.0 mm, hammer vs roller mills |
| Slurry preparation and liquefaction | Starch processing | Jet cookers, SS-lined vessels, steam at 105–110°C |
| Saccharification equipment | Sugar conversion | Enzyme dosing, residence time, pH control |
| Fermentation tanks and yeast propagation | Alcohol fermentation | SS/MS rubber-lined, cooling, CIP, CO₂ venting |
| Distillation columns (multi-pressure) | Ethanol concentration | Trays vs structured packing, heat integration |
| Molecular sieve dehydration unit (MSDH) | Fuel-grade dehydration | 3-Å zeolite, twin-bed PSA, 99.5%+ purity |
| Decanter centrifuges | Wet solids separation | G-force, throughput (m³/hr), wear liners |
| Multiple-effect evaporators (MEE) | Thin stillage concentration | 3–5 effects, steam economy, fouling control |
| DDGS dryer | By-product drying | Steam tube/rotary/ring dryer, outlet moisture 10–12% |
| Boiler and steam generation | Process steam supply | Fuel type (biomass/coal/gas), IBR compliance, ESP |
| Cooling towers and chilled water | Process utilities | Induced-draft, matched to condenser loads |
| Water treatment plant (DM/RO/softening) | Process water quality | Condensate recovery, make-up water reduction |
| Ethanol storage tanks and truck loading | Product storage | SS304/316, ATEX safety, metering systems |
| ETP and optional ZLD systems | Wastewater management | Bio-methanation, RO, evaporation, incineration |
| CO₂ recovery system (optional) | By-product recovery | Scrubbers, compressors, liquefiers |
| PLC/DCS and automation | Process control | Advanced monitoring systems detect leaks and process deviations |
For a multi-feedstock ethanol distillery, additional pre-treatment, storage segregation, and process controls are required. The machinery list is the starting point for CAPEX estimation in a DPR; exact specifications must be customised through detailed process design with the technology licensor or EPC contractor.
Grain Handling, Cleaning & Milling Machinery
Efficient handling of maize, broken rice, and other starch-based crops directly affects plant uptime, contamination risk, and ethanol yield. Promoters developing a maize-based ethanol project or a broken rice ethanol project should pay careful attention to front-end design.
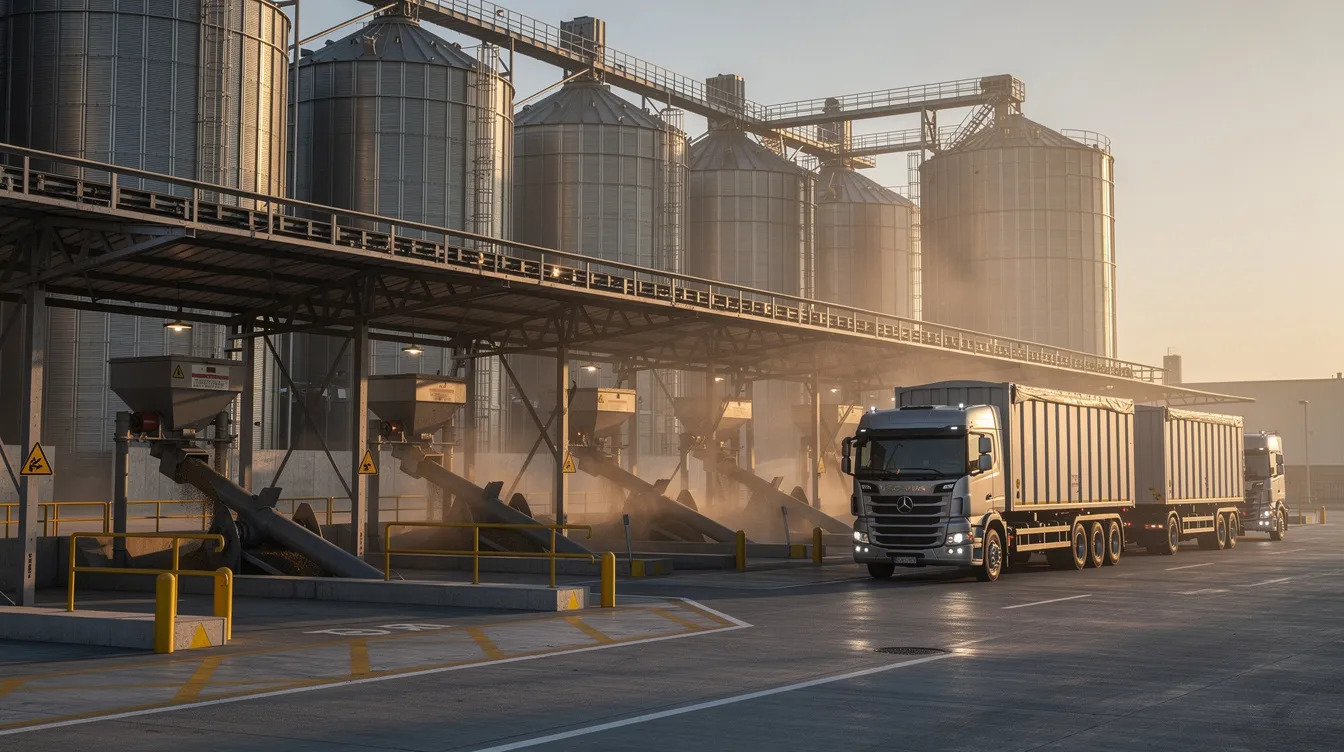
Typical grain unloading arrangements include truck tippers, intake hoppers, belt conveyors, chain conveyors, bucket elevators, magnetic separators, and weighbridges. The layout must support 24–48 hours’ buffer stock for continuous ethanol production. For longer-term storage of 15–30 days’ inventory, RCC godowns or steel silos with aeration and fumigation systems are common – details covered in the grain storage, silos and logistics project report.
Grain cleaning systems – rotary drum cleaners, destoners, aspiration systems, and magnets – remove dust, stones, and ferrous materials. Dust collection, explosion vents, and safety design inspired by ATEX/NFPA standards are essential for fire-hazard control in milling areas.
Milling systems use hammer mills or roller mills to achieve a particle size of approximately 0.5–1.0 mm. Overly fine grinding increases slurry viscosity and pump loads; overly coarse grinding reduces enzyme access to starch. Higher-moisture or damaged grains (FCI surplus broken rice) may need different handling and milling adjustments, affecting operational flexibility. Local feedstock availability and seasonal availability of grains influence storage sizing and procurement strategy, making land acquisition and infrastructure requirements part of the early project management decisions.
Liquefaction, Saccharification & Fermentation Equipment
Conversion of starch to fermentable sugars and onward fermentation is at the heart of ethanol production economics. Starch-based ethanol requires milling, liquefaction, and saccharification – each step affecting litres of ethanol produced per tonne of grain.
Slurry preparation involves slurry tanks, agitators, dosing systems, and jet cookers with steam injection at 105–110°C. Heated slurry in liquefaction tanks uses enzymes to break down starches into sugars. Metallurgy must handle high-temperature cooking, typically requiring SS lining or alloy steel. Liquefaction equipment includes retention columns, viscosity control instruments, and precise temperature and pH monitoring to maximise starch conversion and protect enzyme activity.
Saccharification systems – often combined saccharification-fermentation (SSF) configurations – convert dextrins into fermentable sugars. Advanced enzyme packages can allow lower steam consumption or shorter cycle times, reducing utility costs.
Fermenters are large stainless steel vessels where yeast is added to the mash. Fermentation converts fermentable sugars into ethanol and carbon dioxide using yeast, and fermentation units must maintain stable microbial environments for high yields. For a 200 KLPD plant, several fermenters of 300–400 m³ each may be needed, equipped with cooling coils or external shell-and-tube heat exchangers, CO₂ venting, foam control, and CIP systems. Yeast propagation tanks, nutrient dosing, and instrumentation for temperature, pH, and dissolved oxygen support higher alcohol concentration in the mash.
Liquefaction and fermentation efficiency directly impacts raw materials consumption, ethanol production cost, and sensitivity analysis parameters in a professional feasibility study.
Distillation & Molecular Sieve Dehydration Equipment
Multi-pressure distillation is the main separation system converting fermented wash into fuel ethanol. The distillation process separates ethanol from water and residues based on boiling points. Ethanol distillation requires precise temperature and pressure control, and process design strongly influences steam consumption per litre of ethanol.
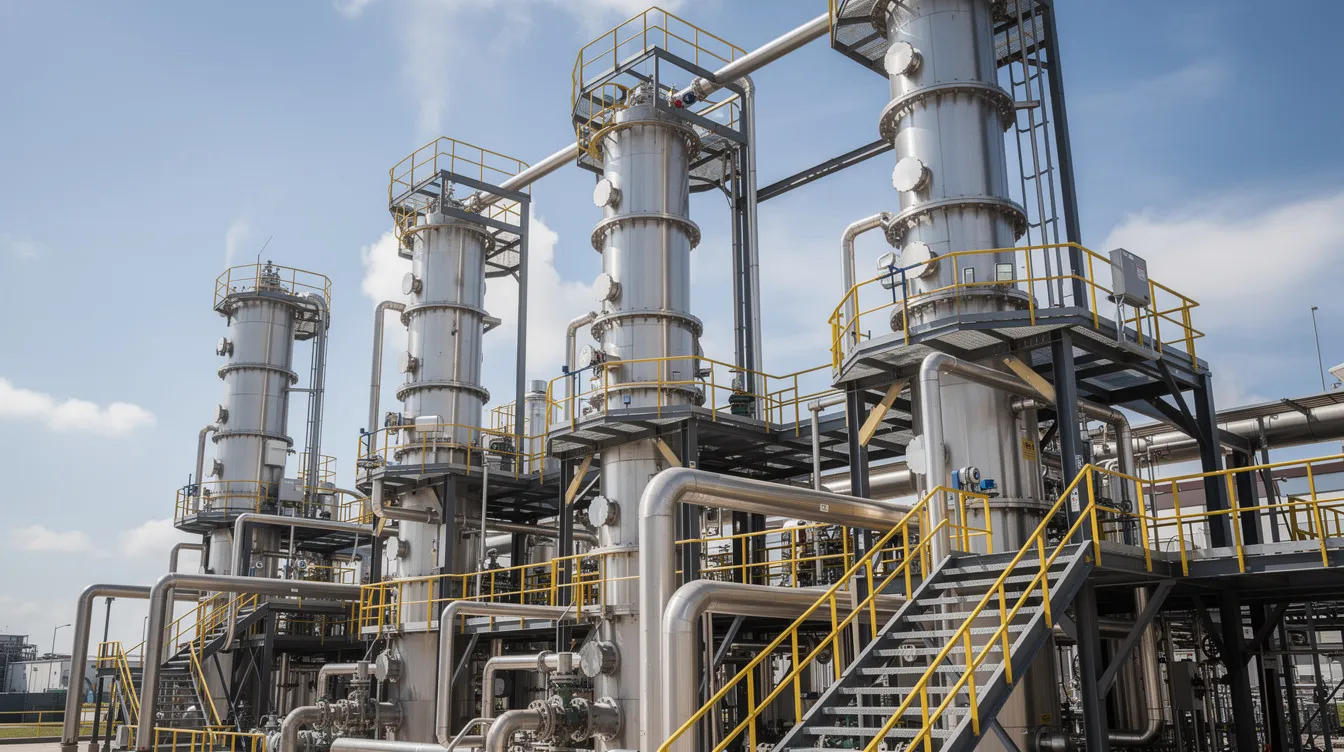
A typical distillation column train for a grain-based ethanol plant includes an analyser column, rectifier column, purifier/head column, fusel oil column, and associated reboilers, condensers, reflux drums, and heat integration exchangers. Multi-column distillation systems optimise ethanol separation efficiency. Selection considerations include the number of columns, operating pressures, structured versus random packing or trays, stainless-steel grades, and integrated heat recovery – for example, using rectifier vapours to heat the analyser feed.
Ethanol forms an azeotrope with water at approximately 95.6% ethanol concentration, meaning conventional distillation alone cannot achieve fuel-grade purity. Molecular sieve dehydration is used to produce anhydrous ethanol by removing residual water. These units employ 3-Å zeolite beads with typical bead sizes of 4×8 mesh, operating on a pressure swing adsorption principle with twin or multi-bed configurations. Zeolite beds in well-designed MSDH units often last 5–7 years before full replacement.
More advanced distillation and MSDH technology can reduce steam consumption and cooling water load, lowering ethanol production cost and improving DSCR – even when initial machinery CAPEX is higher. For a detailed comparison of grain-based versus molasses-based ethanol cost and viability, distillation configuration differences are a key factor.
DDGS Processing, Evaporation & By-Product Equipment
DDGS is a high-protein animal feed produced from the by-products of ethanol manufacturing and is the most valuable co-product in grain-based ethanol plants. DDGS revenue is a major contributor to project profitability and payback period, making it one of the valuable co-products that promoters must plan carefully.
Centrifuges are used to separate wet grains from liquid thin stillage after distillation. Decanter centrifuge selection criteria include throughput capacity (m³/hr), G-force, automation level, and wear protection against abrasive solids. Evaporators concentrate thin stillage into syrup for further processing – typically using 3- to 5-effect MEE systems with careful fouling control and condensate reuse to reduce fresh water demand.
DDGS dryers (steam tube bundle rotary, ring, or flash dryers) reduce outlet moisture to 10–12%, directly affecting product colour, protein quality, storability, and market price. Handling and storage equipment includes DDGS coolers, conveyors, elevators, silos, bagging machines, and dust control systems.
Optional CO₂ recovery systems from fermentation off-gas – scrubbers, compressors, liquefiers, and storage tanks – add CAPEX but can generate additional revenue in favourable local markets. While South America has developed based its ethanol industry largely around sugarcane, Indian grain-based plants benefit from DDGS economics that sugarcane-based facilities do not enjoy.
DDGS recovery efficiency, moisture control, and market realisations (₹/tonne) are critical parameters in financial models. Project Report Bank’s DPRs quantify their impact on project economics, internal rate of return, and mass balance across the plant.
Boilers, Utilities & Environmental Systems
Boilers, power systems, water treatment, and environmental equipment often represent 25–40% of total completed plant cost and strongly influence operating expenses, regulatory approvals, and quality assurance of environmental compliance.
Steam boilers for 60–200 KLPD plants are sized for the required steam throughput, using fuels such as rice husk, coal, biomass briquettes, or natural gas. IBR compliance, ESP or bag-filter emissions control, and fuel handling conveyors are standard requirements. Captive power or cogeneration options – using back-pressure turbines to generate electricity from boiler steam – involve higher CAPEX but reduce grid power purchases and improve operational efficiency.
Cooling towers (induced-draft) are sized to match distillation and MSDH condenser loads. Water treatment systems include raw water softening, RO, DM plants, and condensate recovery to reduce specific water consumption per litre of ethanol and comply with CPCB norms.
Auxiliary utilities include air compressors, electrical distribution (transformers, HT/LT panels, cable networks), plant lighting, earthing, and fire protection (hydrant networks, sprinklers, foam systems). Ethanol production requires compliance with local zoning laws, and effluent treatment systems minimise environmental impact and ensure compliance.
Ethanol plants must implement Zero Liquid Discharge for effluent management in most new projects. Environmental Clearance under EIA Notification 2006 can take 12–18 months to obtain. ETP and ZLD systems – bio-methanation, RO, evaporation, incineration – must be engineered in parallel with process design. The final scheme depends on local regulations, water availability, and specific requirements of the state pollution control board. Budgeting these systems correctly is vital for realistic CAPEX estimates and lender appraisals.
Ethanol Distillery Machinery Cost in India
This section presents indicative budgeting norms based on recent Indian projects up to FY 2025–26. These figures are not substitutes for vendor quotations or a formal feasibility study.
Ethanol distillery machinery cost must be understood at three levels: (a) ex-works equipment price from the manufacturer, (b) installed plant machinery cost including freight, GST (~18%), erection, piping, insulation, and instrumentation, and (c) total project investment including civil works, buildings, utilities, IDC, pre-operative expenses, and working capital margin. Grain-based plants have higher capital costs due to grain handling systems compared to molasses-based facilities.
The following table presents a machinery-wise cost breakdown for a reference 100 KLPD grain-based ethanol manufacturing plant:
| Machinery Section | Equipment Included | Indicative Cost (₹ Crore, Installed) | Key Cost Drivers |
|---|---|---|---|
| Grain handling and milling | Cleaners, conveyors, hammer mills, silos | 10–15 | Capacity, automation level, storage days |
| Liquefaction and fermentation | Slurry tanks, jet cookers, fermenters, HX | 20–25 | Metallurgy, number of fermenters, cooling |
| Distillation and dehydration | Column train, MSDH, reboilers, condensers | 25–35 | Steam integration, packing type, beds |
| DDGS and evaporation | Decanters, MEE, dryers, conveyors | 10–18 | MEE effects, dryer type, DDGS output |
| Boilers and utilities | Boiler, fuel handling, cooling towers, WTP | 20–30 | Fuel type, cogeneration, capacity |
| Electrical and automation | PLC/DCS, panels, cabling, instruments | 7–12 | Integration scope, redundancy |
| Storage, loading, and safety | Ethanol tanks, truck loading, fire systems | 3–6 | Tank volume, safety classification |
| Effluent and environmental | ETP, ZLD systems, bio-methanation | 8–15 | ZLD requirement, discharge norms |
These ranges sum to approximately ₹103–156 crore for installed machinery and auxiliaries. As per ICRA research, setting up a 1G ethanol plant in India costs around ₹1.30–1.60 crore per KLPD, of which 71–76% is plant and machinery. For context, the SLB Ethanol 200 KLPD project reported process plant machinery at ₹98 crore, boiler and turbine at ₹31.90 crore, and electrical/instrumentation at ₹36.25 crore – totalling approximately ₹148 crore for machinery, within a total cost of ₹270.20 crore including IDC and working capital.
Major cost drivers include plant capacity (KLPD), feedstock type requiring different front-end equipment, energy-efficiency features, ETP/ZLD configuration, and the extent of cogeneration. GST, freight, erection, commissioning, and contingencies (typically 5–10%) must be budgeted separately. For a complete understanding of how machinery cost fits within total project cost – including land, civil, infrastructure requirements, and IDC – refer to the detailed guide on grain-based ethanol plant setup cost in India.
Machinery Cost Comparison – 60, 100 & 200 KLPD Ethanol Plants
Machinery cost per KLPD does not scale linearly. Larger plants benefit from economies of scale on shared systems, but utilities and environmental systems scale more directly with throughput.
| Parameter | 60 KLPD | 100 KLPD | 200 KLPD |
|---|---|---|---|
| Grain throughput (approx. TPD) | 160–180 | 270–300 | 540–600 |
| Fermenters (indicative number) | 4–6 | 6–8 | 10–14 |
| DDGS output (approx. TPD) | 50–55 | 85–100 | 170–200 |
| Boiler capacity (indicative) | 12–16 TPH | 20–28 TPH | 40–55 TPH |
| Installed machinery cost (₹ Crore) | 65–95 | 100–150 | 150–220 |
| Machinery cost per KLPD (₹ Crore) | 1.10–1.60 | 1.00–1.50 | 0.75–1.10 |
| Expansion flexibility | Limited | Moderate | High with debottlenecking |
A 60–100 KLPD molasses-based plant costs INR 50–150 crore – substantially lower than grain-based plants at similar capacity, primarily due to simpler feedstock preparation. Certain fixed-cost items (control room, laboratory, substation) do not scale fully with capacity, improving per-KLPD CAPEX for larger units. The Coastal Corporation’s approved 300 KLPD ethanol plant in Odisha at approximately ₹350 crore implies about ₹1.17 crore per KLPD at that scale.
Promoters considering future expansion – say designing a 100 KLPD plant with provision to upgrade to 160 KLPD – should address this at the engineering stage to avoid expensive retrofits. Total cost considerations should always include civil works, land acquisition, and pre-operative expenses alongside the machinery package.
Indian vs Imported Ethanol Distillery Machinery
India has capable domestic EPC contractors and OEMs providing grain-based ethanol plant machinery, many with licensed or proprietary process technology. Domestic suppliers often offer complete plant packages from process design through commissioning, with shorter lead times and local service.
However, some specialised components – molecular sieve valves, advanced instrumentation, certain distillation internals – may be sourced from overseas. Technology licensing models vary: some Indian players manufacture most equipment locally while licensing the core process flowsheet.
Practical considerations when comparing Indian and imported machinery:
- CAPEX differences driven by exchange rate, import duty, freight, and local fabrication advantages
- Lead times and shipping risks for imported components
- Automation level, energy efficiency, and digitalisation features
- Availability of local spare parts and service response time
- Warranty enforcement complexity with overseas suppliers
- Performance guarantees covering ethanol yield, steam and power consumption, and DDGS quality
Promoters should evaluate total lifecycle cost (CAPEX plus OPEX plus downtime risk) rather than comparing only initial machinery prices. Lenders may look more favourably at suppliers with a proven track record in India, particularly for manufacture and commissioning of large-capacity plants. A renewable energy context and environmental compliance track record also matter to credit appraisers.
How Machinery Selection Impacts Project Financial Viability
From a project finance advisory perspective, machinery selection is a financial decision – not merely an engineering one. Profitability depends on the interplay between CAPEX, operating efficiency, and revenue realisation.
Higher-efficiency machinery increases initial CAPEX but can reduce steam, power, and chemical costs per litre, improving EBITDA margins. Gross profit margins for ethanol plants typically range from 20–30%, and feedstock costs account for 70–80% of operating expenses. Even small improvements in ethanol recovery or steam consumption meaningfully affect profitability.
Higher machinery cost leads to a larger term loan amount, higher interest during construction (IDC), and requirement of stronger promoter contribution. Typical debt–equity ratios and capital subsidies or interest subvention under government schemes influence the means of finance structure. Reliable machinery leading to stable capacity utilisation (80–90% versus 60–65%) produces smoother cash flows and less strain on working capital limits.
Ethanol projects target an internal rate of return of 15–20%, with typical payback periods of 6–9 years. Operating costs increase significantly by the fifth year of operation due to maintenance and replacement cycles. Project economics must be tested through sensitivity analysis covering variations in feedstock cost, DDGS price, steam consumption, and capacity utilisation. These insights provided through financial projections and modelling help promoters and lenders understand financial robustness.
A cheaper quotation with poor energy efficiency, unreliable performance, or weak guarantees can reduce IRR and fail lender stress tests once realistic operating costs are modelled. Promoters should commission a formal project feasibility study before finalising machinery orders, aligning engineering decisions with bankability.
Machinery Supplier Selection & EPC Contract Checklist
Ethanol distillery projects are capital-intensive – often ₹150–400 crore or more in total investment. Supplier and EPC selection is a long-term partnership decision affecting project management quality and company reputation.
Key evaluation criteria:
- Proven experience with grain-based ethanol projects in India and recent reference installations
- Clarity on process technology: proprietary or licensed flowsheet, expected yields, energy consumption guarantees
- Performance guarantees for ethanol output per tonne of grain (typically 380–400 litres per MT of maize), steam and power consumption, DDGS moisture and protein quality
- Detailed machinery scope, battery limits, and exclusions (civil, structural steel, piping, insulation, cabling)
- Engineering deliverables: PFDs, P&IDs, equipment GA drawings, plant layout, instrument lists, and control philosophy
- Supply, erection, and commissioning responsibilities with clear milestones
- Performance test protocols, acceptance criteria, trial-run procedures
- Warranty period, spare parts package, and operator training
- Delivery schedule tied to project implementation plan
- Payment milestones linked to manufacturing progress, dispatch, erection, and successful performance tests
- Liquidated damages for delay or performance shortfall
Promoters should compare bids on a like-to-like basis using a standardised technical and commercial comparison sheet. For multi-feedstock ethanol plants, define performance guarantees separately for each feedstock combination. Ethanol plant setup typically takes 30–48 months from concept to production, and procurement to commissioning of major machinery often takes 14–20 months after order placement.
Machinery Cost Considerations for Bank Loan DPR
Accurate ethanol distillery machinery estimates form the backbone of a bankable Detailed Project Report (DPR). Lenders scrutinise these numbers during technical and financial appraisal.
Project Report Bank typically incorporates machinery cost into DPRs by collecting formal supplier quotations or budgetary offers, preparing fixed-asset schedules separating process plant, utilities, electrical, civil, and other assets, and allocating installation, freight, taxes, and contingencies into machinery-related CAPEX. The total cost must be developed based on actual project scope.
Integration into means of finance includes promoter contribution planning, term loan sizing, possible subsidies or interest subvention under government schemes, and loan structuring. Key financial assumptions linked to machinery include useful life, depreciation rates, implementation period (and hence IDC), trial-run losses, and ramp-up in capacity utilisation used in financial projections.
Working capital assessment must account for grain inventory, finished ethanol stock, DDGS stock, receivables from OMCs or industrial buyers, and how machinery-driven cycle time and reliability affect these balances. Raw materials account for 70–80% of operating expenses, making production reliability critical to cash flow.
DSCR, break-even capacity utilisation, IRR, and payback period are all sensitive to actual installed machinery performance and costs. Promoters should engage early with professional DPR and CMA Data preparation experts through bank finance DPR and loan proposal assistance to align machinery choices, project economics, and financing structure before finalising orders.
Frequently Asked Questions
The following FAQs address additional machinery and finance queries commonly raised by first-time ethanol plant promoters in India.
What basic machinery is required for a 100 KLPD grain-based ethanol plant?
A 100 KLPD plant requires grain intake and milling equipment, slurry preparation and liquefaction systems, saccharification and fermentation vessels, multi-column distillation, molecular sieve dehydration, DDGS processing (decanters, MEE, dryer), boilers and utilities, ETP or ZLD systems, ethanol storage and loading systems, and plant-wide PLC/DCS automation. Within each section, multiple individual items must be sized consistently to maintain mass balance and throughput.
How early should ethanol distillery machinery vendors be finalised?
Technology and vendor shortlisting should begin during the feasibility study, with budgetary offers used to build the DPR. Detailed engineering and firm purchase orders typically follow financial closure, often 6–9 months before targeted mechanical completion, to align manufacturing and delivery schedules with bank disbursements.
Can the same ethanol distillery machinery handle both maize and broken rice?
From liquefaction onwards, most grain-based ethanol distillery equipment can handle multiple grains. However, front-end handling, cleaning, milling settings, and enzyme packages may need adjustment for different grain types. A properly designed multi-grain plant includes flexible milling configurations and process controls to produce alcohol from varying grain mixes.
Is it possible to start with 60 KLPD machinery and later expand to 100 KLPD?
Staged expansion is feasible if planned from day one. Certain shared systems – ETP, control room, substation, some storage – can be overdesigned for the target capacity. Modular fermenters, additional distillation capacity, and boiler modules are added during expansion. Unplanned expansion is usually more expensive and disruptive to ongoing production.
How does energy-efficient ethanol distillery machinery improve plant profitability?
Energy-efficient machinery – low-steam distillation, higher-effect MEE, heat-integrated column designs – reduces steam consumption from 4.5 to as low as 3.0 kg per litre. This directly lowers fuel cost per litre of ethanol produced. Over a 10-year horizon, the OPEX savings from efficient machinery can substantially exceed the incremental CAPEX, improving EBITDA, DSCR, and overall project viability.
Conclusion – Choosing Machinery for a Bankable Ethanol Project
Ethanol distillery machinery selection is not just a technical exercise – it is a financial decision shaping total CAPEX, ethanol production cost, DDGS revenue, and long-term plant viability. Promoters should evaluate technology efficiency, energy consumption, by-product handling, environmental compliance, and supplier track record together, rather than focusing only on the lowest machinery price.
Bankable project economics depend on realistic machinery costs, robust financial projections, and sensitivity analysis covering feedstock, energy, and capacity utilisation risks. The interplay between machinery performance and financial outcomes – DSCR, IRR, break-even, and payback – determines whether a project secures finance and delivers returns.
Serious entrepreneurs and industrial investors planning grain-based, molasses-based, or multi-feedstock ethanol projects are welcome to engage Project Report Bank for customised DPRs, financial modelling, CMA Data, and bank loan proposal support. Professional advisory by CA Manish Gugliya ensures that machinery choices, project economics, and financing structure are aligned from the outset.